Quick Answer
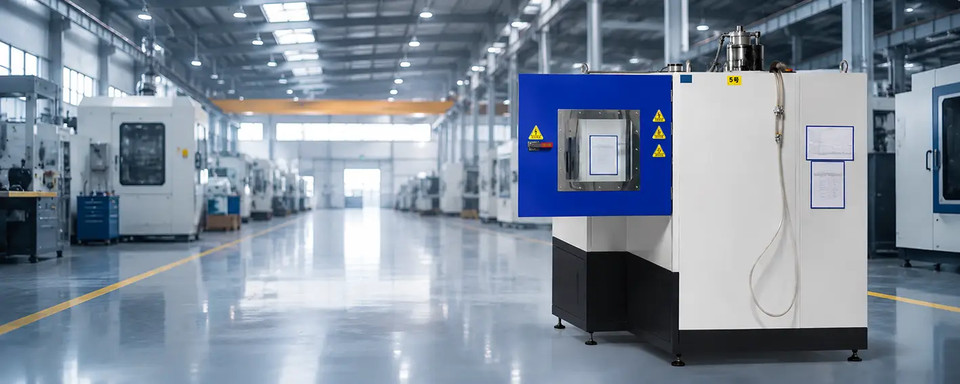
A batch wet blasting machine is usually the best fit when manufacturers need controlled surface treatment on repeat parts without committing to a fully inline layout. It combines water, abrasive media, and compressed air inside an enclosed cabinet or chamber to deliver cleaner blasting, more consistent finishes, and lower airborne dust than dry blasting. In practice, batch systems are widely used for deburring, edge honing, scale removal, coating pretreatment, and cosmetic finishing where part handling is cyclical rather than continuous and process repeatability matters more than maximum line speed.
| Core Factor | Typical Conclusion |
|---|---|
| Process type | Enclosed wet abrasive blasting for batch-loaded parts |
| Operating mode | Manual, semi-automatic, or servo-assisted chamber processing |
| Dust behavior | Low airborne dust relative to dry blasting because water suppresses fines |
| Best-fit production level | R&D, mixed-part production, small to medium batches |
| Common applications | Deburring, edge honing, pretreatment, oxide removal, matte finishing |
| Typical project lead time | Standard batch systems are typically shorter than custom line-integrated systems |
What Is Batch Wet Blasting Machine
A batch wet blasting machine is an enclosed industrial surface treatment system designed to process a group of parts, or one fixture load of parts, in discrete cycles rather than in a continuous line flow. Operators load the workpieces into a chamber, run the programmed or manual blasting cycle, then unload the finished batch before starting the next cycle. That structure makes the machine particularly suitable for factories handling multiple SKUs, variable part sizes, and moderate throughput requirements.
Within the larger wet blasting, slurry blasting, and vapor blasting family, the batch format is defined by its production logic. The surface treatment mechanism remains the same as other wet blasting systems: abrasive particles are suspended in water, delivered as slurry, and accelerated by compressed air toward the workpiece. The difference lies in how parts are presented, how the cycle is controlled, and how one batch is separated from the next.
This format occupies an important middle position between small manual blasting cabinets and fully integrated inline systems. A batch wet blasting machine can be compact enough for flexible job-shop use, but sophisticated enough to support fixture-based repeatability, recipe storage, servo nozzle motion, and controlled pressure windows. For many manufacturers, that balance is the reason batch equipment remains a practical investment.
The process sits inside the broader category of [abrasive blasting terminology], but wet blasting uses water as the carrier phase that changes both environmental behavior and surface interaction. Instead of creating a dry plume of spent media and fines, the process keeps the abrasive in suspension, reducing airborne dust and often improving housekeeping in comparison with dry blasting rooms or cabinets.
Key selling points are technical rather than cosmetic. Water suppresses dust generation. The water film can reduce the risk of abrasive embedding on many sensitive surfaces. Impact is often more cushioned than dry blasting, which helps support a finer and more uniform finish. Most importantly for batch production, process variables such as pressure, slurry concentration, nozzle path, stand-off, and dwell time can be held within a stable operating window from one load to the next.
For that reason, batch wet blasting machines are widely used where parts cannot simply be “cleaned aggressively” and sent on. They are chosen where surface condition affects downstream coating adhesion, cutting-edge performance, cosmetic appearance, dimensional consistency at sharp features, or fatigue-related surface behavior. In other words, the batch system is not only a cleaning cabinet; it is a controlled finishing process.
How Does Batch Wet Blasting Machine Work
A batch wet blasting machine works by preparing a slurry of water and abrasive, pumping that slurry to blast nozzles, accelerating it with compressed air, directing it at the loaded workpieces inside a sealed chamber, and then recovering the spent slurry for recirculation and waste separation. Although the process sounds straightforward, each stage affects finish quality, media life, and batch-to-batch consistency.
Slurry Mixing and Wet Sandblasting Media Suspension
The process begins in the slurry tank or sump, where water and abrasive are mixed into suspension. Agitation or circulation is used to keep the media distributed evenly so that heavier particles do not settle excessively before reaching the blast guns. In a well-designed system, the slurry is not treated as static liquid; it is a controlled process medium whose concentration and cleanliness must remain stable during the blasting cycle.
Media selection is one of the most important setup decisions. Fine media are commonly used for delicate deburring, edge preparation, cosmetic texturing, and sensitive substrates. Coarser media are more appropriate where the objective is heavier scale removal or stronger surface conditioning. The right choice depends on substrate hardness, part geometry, finish target, and allowable erosion rate.
Compressed Air Acceleration and Surface Impact
The slurry is circulated to the blast gun or nozzle assembly, where compressed air accelerates the media-water mixture toward the workpiece. Surface interaction is controlled by pressure, nozzle bore, impact angle, stand-off distance, exposure time, and media particle size. In batch equipment, those variables may be adjusted manually, semi-automatically, or by stored recipe.
Because the workpieces are enclosed in a chamber, the operator or machine can focus energy more precisely on the required zones. That is a key advantage over broader mass-finishing methods. A batch wet blasting machine can target edges, holes, faces, pockets, or cosmetic surfaces without subjecting the entire part to the same uncontrolled treatment.
Chamber Process, Part Handling, and Repeatability
Part loading style varies by machine type. Simpler units may rely on manual placement or hand-held gun work. More advanced systems use rotating fixtures, indexed part holders, or servo-driven X/Y/Z nozzle movement to maintain stable exposure over the same workpiece geometry every cycle. This is where batch equipment becomes more than a cabinet: it becomes a repeatable process cell.
When parts require a consistent edge radius, selective burr removal, or uniform matte finish, repeatable presentation is often more important than maximum blast pressure. Stable fixture location, predictable rotation, and synchronized nozzle movement reduce variance between the first batch and the next. That directly affects scrap risk, rework, and process qualification.
Closed-Loop Recovery, Sedimentation, and Mist Extraction
After the abrasive hits the part, the used slurry drains back into the machine’s recovery circuit. Reusable media and water are recirculated, while fines, contaminants, and broken particles are removed gradually through settling, screening, or waste-sand discharge. This closed-loop slurry recovery is one of the defining features of industrial wet blasting because it makes media use more economical and helps maintain a more predictable process over time.
Although wet blasting greatly reduces dry airborne dust, it still requires ventilation and mist control. Water mist, splash, and fine suspended contaminants must be managed so that cabinet visibility remains good and surrounding equipment is protected. For that reason, production-grade machines often include dedicated extraction and drainage design rather than relying on the water phase alone.
PID Pressure Control and Recipe Management
Pressure stability matters because surface results often change noticeably when blast energy drifts. Batch systems with PID pressure control monitor and regulate blasting conditions more tightly than ad hoc manual adjustment. That is especially important for edge honing, coating pretreatment, or cosmetic finishing programs where an overly aggressive cycle can alter the part beyond specification.
Recipe management adds another layer of control. Operators can store settings for pressure, nozzle motion, batch time, fixture sequence, and other variables by part family. That reduces setup variation and makes the batch wet blasting machine more suitable for mixed-product environments.
In batch wet blasting, repeatability depends less on peak aggressiveness than on keeping slurry, pressure, and part presentation inside a controlled process window.
| Process Parameter | Typical Batch Practice | Why It Matters |
|---|---|---|
| Working pressure | Typical wet blasting operates in a controlled low-to-medium pressure band set by application | Balances removal rate, finish quality, and substrate protection |
| Slurry concentration | Typically maintained within a defined media-to-water ratio | Controls cutting action, finish consistency, and media stability |
| Abrasive particle size | Fine to medium particle distributions are typical, depending on the task | Influences texture, edge response, and cleaning intensity |
| Air flow demand | Sized to nozzle count, nozzle diameter, and duty cycle | Prevents pressure collapse during sustained blasting |
| Media consumption rate | Depends on contamination load, media breakdown, and recovery efficiency | Affects operating cost and maintenance interval |
| Control system | Manual adjustment, PLC/HMI recipes, or PID-regulated pressure control | Determines repeatability and ease of changeover |
Batch Wet Blasting Machine vs Dry Blasting vs Other Methods
A batch wet blasting machine is often compared with dry blasting, shot peening, and vibratory finishing because all four can change the surface of a part. The important distinction is that they do so in different ways and are optimized for different production goals.
Dry blasting is usually selected for aggressive cleaning, rust removal, and large-scale roughening where dust collection infrastructure is already in place and the substrate can tolerate a harsher process. Shot peening, described broadly through [shot peening terminology], is not primarily a cleaning process at all; it is used to modify surface stress conditions for fatigue-related performance. Vibratory finishing, by contrast, is a mass-finishing method that can smooth and soften edges across many small parts at once, but it is generally less selective than nozzle-based blasting.
Batch wet blasting becomes attractive when the factory needs better surface control than dry blasting typically offers, more local selectivity than vibratory methods can provide, and a cleaner chamber environment than open dry processes. It is especially relevant in tool manufacturing, precision deburring, cosmetic finishing, and coating-prep workflows shaped by [surface preparation guidance].
| Evaluation Dimension | Batch Wet Blasting | Dry Blasting | Shot Peening | Vibratory Finishing |
|---|---|---|---|---|
| Airborne dust generation | Low relative to dry blasting because water suppresses fines | High unless extraction is very robust | Moderate in enclosed cells | Low external dust, but wet compounds and media must be handled |
| Surface finish character | Fine, uniform, and controllable on many precision parts | Often more aggressive and rougher by comparison | Texture is secondary to stress effect | Broad smoothing across exposed surfaces |
| Media embedding risk | Reduced on many soft or coated substrates | Higher on some sensitive materials | Depends on media and substrate pairing | Not a blasting mechanism, so not directly equivalent |
| Local treatment control | High with nozzles, fixtures, or servo motion | High, but often with more dust burden | Moderate to high in dedicated peening setups | Lower for selective local features |
| Best-fit application | Deburring, edge honing, pretreatment, cosmetic texture | Rust removal, cleaning, heavy roughening | Fatigue-related surface conditioning | Bulk smoothing and edge softening |
| Environmental profile | Cleaner chamber atmosphere, but slurry waste must be managed | More dust and dry waste handling | Dry contained process with media control needs | Liquid compounds and media disposal required |
Key Specifications to Evaluate Before Buying
Choosing a batch wet blasting machine starts with understanding the actual process objective. Some buyers ask first about machine size, but chamber dimensions alone say very little about whether the equipment can deliver consistent edge preparation, selective deburring, or coating-ready finishes. The critical issue is whether the machine can keep the full process stable from batch to batch.
Blasting Pressure, Slurry Concentration, and Process Window
Pressure should be evaluated as a controllable operating range rather than as a maximum headline number. Many precision blasting jobs require moderate but stable pressure instead of peak aggressiveness. Buyers should ask how pressure is measured, whether the machine uses feedback control, and how nozzle wear affects actual blasting energy over time.
Slurry concentration control is equally important. If the media-to-water ratio drifts between batches, the finish, removal rate, and edge effect can shift with it. A procurement review should therefore include agitation method, concentration correction logic, and the way the system handles fines, broken media, and removed material.
Motion Accuracy and Part Presentation
A batch wet blasting machine may use manual gun handling, rotary tables, fixture indexing, or servo-driven motion. The right choice depends on how sensitive the part is to exposure angle and dwell time. For repeat production of technical components, fixturing and motion control often have more impact on result consistency than raw pressure capacity.
If the supplier offers servo linkage, buyers should verify the claimed motion accuracy at the actual blasting point, not only in unloaded axis travel. On complex parts, a stable nozzle path is essential for consistent treatment of edges, recesses, and formed surfaces. This is where repeatable batch processing becomes a measurable engineering requirement rather than a marketing phrase.
Throughput, Cycle Time, and Changeover Logic
Throughput should be defined in finished parts per shift for the real part mix, not in an abstract chamber cycle. Some machines can process large batches, but loading, masking, fixture change, drying, and unloading may dominate total cycle time. The supplier should help map the true operational sequence.
Changeover time matters when the production mix is varied. Recipe recall, quick-change fixtures, and clear HMI logic can significantly reduce lost time between part families. For factories that run frequent short batches, this may be more important than maximum chamber size.
Utility Demand, Footprint, and Maintenance Access
Compressed air demand, electrical load, water management, drainage, and mist extraction all need early review. Wet blasting is cleaner than dry blasting in terms of airborne dust, but it still requires careful handling of slurry circulation and water mist. The machine footprint should therefore include service clearance, sludge access, and maintenance zones.
Buyers should also inspect how easy it is to reach pumps, hoses, nozzles, windows, and waste-discharge points. A batch wet blasting machine that is difficult to clean or service will often lose process consistency over time because preventive maintenance becomes inconvenient.
HMI, Safety, and Data Control
The HMI should do more than start and stop the cycle. In modern production, operators benefit from stored recipes, alarm records, usage counters, permission levels, and maintenance reminders. These features matter especially when a plant is running multiple operators or multiple work shifts.
Safety review should include door interlocks, emergency stops, visibility, drainage integrity, cabinet sealing, and extraction performance. On more advanced systems, waste-sand handling and mist control should be assessed as part of safe routine operation, not as optional extras. The most reliable systems are built around process-window stability, not around manual adjustment after problems appear.
A practical procurement checklist should cover these points:
- Confirm part size range, weight, and fixture method.
- Define whether the machine will be manual, semi-automatic, or servo-assisted.
- Review blasting pressure control and slurry concentration management.
- Verify nozzle access to critical features and recessed surfaces.
- Evaluate cycle time, loading time, and changeover time together.
- Check compressed air flow, drainage, and extraction requirements.
- Confirm HMI recipe storage and hierarchical permission settings.
- Ask how waste-sand sedimentation and discharge are handled.
- Review maintenance access to pumps, nozzles, seals, and viewing windows.
- Match the machine architecture to real production mix rather than theoretical maximum capacity.
Applications Across Industries
Batch wet blasting machines are used across industries because they can process different part families without requiring a fixed inline layout. That flexibility makes them especially useful where production runs are repetitive but not fully continuous, or where finish requirements change across product types.
In the cutting-tool sector, [edge honing of cutting tools] is a common use case because the process can refine edge condition without relying on purely manual handling. For machining and stamping suppliers, [burr removing of metal parts] is often a better fit for a batch wet blasting machine than mass finishing when only specific surfaces or burr zones need attention.
Batch systems also play a practical role in coating workflows. Surface preparation before painting or conversion coating frequently benefits from controlled wet blasting, and [coating pretreatment wet blasting] is relevant where substrate uniformity matters more than maximum roughening speed. In broader industrial finishing, the same machine concept is used for forged parts, additive-manufactured components, glass, and consumer-device housings.
| Application Type | Target Industry | Workpiece Example | Process Benefit |
|---|---|---|---|
| Edge honing | Cutting tool manufacturing | Carbide inserts, drills, end mills | Controlled edge preparation and more repeatable edge condition |
| Burr removal | Precision machining, stamping | Brackets, valve components, machined housings | Selective deburring with consistent surface finish |
| Scale removal | Forging and steel processing | Forgings, heat-treated parts, steel bars | Even oxide and scale removal before downstream finishing |
| Pretreatment before coating | Automotive supply, hardware, fabricated metal | Shelves, brackets, shells, structural parts | Cleaner, more uniform substrate before coating |
| AM post-processing | Additive manufacturing | Metal printed parts with complex surfaces | Smoother finish and improved removal of residual surface contamination |
| Light peening / conditioning | Mechanical components | Functional metal parts requiring controlled impact | Stable surface conditioning in an enclosed process |
| Glass frosting | Technical and decorative glass | Panels, covers, specialty glass parts | Uniform matte appearance and lower dry-dust burden |
| 3C device finishing | Electronics and consumer devices | Frames, covers, enclosures | Cosmetic texture control and improved surface feel |
Equipment Selection Guide
Selecting the right batch wet blasting machine means matching chamber type, motion system, and part handling to the actual production pattern. Not every batch process needs robotics, and not every manual cabinet is sufficient for precision work. The most suitable choice usually depends on whether the user values flexibility, throughput, feature-specific control, or large-workspace capacity.
Matching Batch Wet Blasting to Production Scale
For early-stage process development or frequent product variation, flexible R&D-style equipment is often preferred. A machine such as the RB-6 R&D blasting cell is more suitable for sample trials, parameter studies, and multi-part experimentation than for routine repetitive output. Once the process is validated, many manufacturers shift to a dedicated production chamber.
A standard production format may be closer to the SC-40 batch wet blasting cabinet, which suits discrete-cycle loading and unloading for regular shop-floor use. If one part at a time must be handled with strong orientation control, a single-piece blasting machine can make more sense than a loose mixed-part chamber.
Geometry-Specific and Higher-Output Batch Configurations
Part geometry is often the deciding factor. Complex shapes may need servo axes or tailored gun paths, while flat parts can benefit from specialized presentation. For factories transitioning toward higher-volume chamber-based output, a double-chamber blasting system may improve utilization by overlapping loading and blasting functions even though the process remains fundamentally batch-oriented.
| Configuration / Model Tier | Target Production Scale | Workpiece Size Range | Precision Level | Recommended Applications |
|---|---|---|---|---|
| 1. Bench sample unit | Lab and trial work | Very small parts | Moderate | Abrasive screening and early process checks |
| 2. Flexible R&D robotic cell | Development and sample validation | Small precision parts | High | Process trials, multi-angle blasting, recipe validation |
| 3. Manual cabinet batch system | Small-lot production | Small to medium parts | Moderate | Cleaning, simple deburring, matte finishing |
| 4. Standard single-chamber production cabinet | Small to medium batch production | Small to medium parts | High | Routine deburring, pretreatment, edge preparation |
| 5. Single-piece dedicated chamber | Repetitive discrete-part production | Medium parts | High | Controlled blasting of one oriented part per cycle |
| 6. Servo multi-axis batch machine | Precision and complex geometry | Small to medium complex parts | Very high | Selective feature treatment and controlled edge work |
| 7. Large-workspace batch chamber | Larger fabricated components | Medium to large parts | Moderate to high | Coating prep, scale removal, surface conditioning |
| 8. Double-chamber high-utilization system | Repetitive higher-output batches | Small to medium repeat parts | High | Overlapped load/blast/unload for better equipment utilization |
Cost, Lead Time and ROI Considerations
The cost of a batch wet blasting machine depends first on machine architecture and second on the degree of automation built around that architecture. A simple manual cabinet, a servo-assisted production chamber, and a double-chamber high-utilization system may all use the same basic blasting principle, but their cost structures differ because motion control, fixturing, extraction, HMI complexity, and maintenance design differ.
One major price driver is how controlled the process needs to be. If the application only requires general cleaning, the machine can be relatively simple. If the buyer needs edge conditioning, fixture-based repeatability, controlled nozzle paths, and recipe-managed changeovers, the system becomes more engineering-intensive. That is especially true where process validation must be documented across multiple part families.
A second cost driver is slurry management. Better agitation, recovery, sedimentation, and waste handling usually increase initial equipment cost, but they also improve long-run stability. For many buyers, that tradeoff is worthwhile because inconsistent slurry condition is one of the most common causes of finish drift and maintenance-related downtime.
Lead time should be treated as typical rather than guaranteed. Standardized batch machines are generally faster to deliver than highly customized systems with unique fixturing, motion paths, or integrated handling. Lead time extends further when the project includes sample validation, custom utilities, export documentation, or on-site commissioning planning.
ROI for a batch wet blasting machine is normally built from several operational improvements rather than one isolated metric. The first is labor efficiency: a controlled chamber process often reduces manual finishing effort and lowers operator-to-operator variation. The second is quality consistency, especially where burr removal, cosmetic texture, or coating pretreatment affects downstream yield.
Other ROI sources are application-specific. Cutting-tool producers may value more stable edge preparation. Coating lines may see fewer adhesion-related defects. Precision part suppliers may reduce rework because the blasting process is no longer improvised. Mixed-product shops may benefit from faster changeover and less floor contamination than a comparable dry blasting setup.
The strongest business case usually appears where a plant is caught between two inefficient options: manual hand-finishing that is too variable, or fully inline automation that is too rigid or expensive for the current product mix. In that middle zone, the batch wet blasting machine provides controllable finishing without requiring continuous-flow production logic.
Why Choose DasiAuto?
Established in 2012, DasiAuto develops and manufactures wet blasting equipment for industrial surface treatment. The company brings together equipment engineering, abrasive media, and application development, as described in About DasiAuto.
Application testing and process development help evaluate abrasive media and treatment settings before the equipment configuration is defined. Equipment engineering can bring together the blasting system, fixtures, automation, and part handling around the application.
Suitability for a particular material, geometry, finish, or dimensional requirement needs to be established through representative sample testing. DasiAuto supports installation, operator training, and ongoing technical support through the production workflow.
FAQ
Is a Batch Wet Blasting Machine Suitable for Mixed-Part Production?
Yes. A batch wet blasting machine is often chosen specifically because it can handle changing part families more easily than a fully inline system. With proper fixtures, recipes, and operator procedures, it can support repeatable processing across small and medium production lots.
Can Sample Testing Be Done Before Ordering a Production Machine?
Sample testing is generally advisable, especially for edge honing, deburring, cosmetic finishing, or coating pretreatment. Trial work helps determine abrasive grade, slurry concentration, pressure window, nozzle angle, and whether manual, fixture-based, or servo-assisted handling is more appropriate. That information reduces risk before final machine configuration is frozen.
What Should a Buyer Provide When Requesting a Quotation?
Useful inputs include part drawings, material type, dimensions, current process, target finish, expected batch size, and desired throughput per shift. Photos of typical burrs, edges, or surface defects are also helpful. The better the process definition, the more accurately the supplier can match chamber size, nozzle layout, and utility requirements.
How Difficult Is Installation and Operator Training for a Batch Wet Blasting Machine?
Installation is usually simpler than a line-integrated wet blasting system, but it still requires attention to compressed air, power, drainage, and extraction. Operator training should cover not only machine operation, but also slurry maintenance, nozzle inspection, media management, safety interlocks, and recipe use. Good training matters because wet blasting consistency depends on controlled routine practice.
What Spare Parts and Consumables Should Be Planned From the Beginning?
Typical planning should include blasting media, nozzles, hoses, seals, viewing-window protection items, and pump-related wear components. Depending on the machine, users may also need replacement filters, sediment handling items, and fixture consumables. A realistic consumables plan helps keep the batch wet blasting machine running within the intended process window.
How Should Warranty and After-Sales Support Be Evaluated?
Warranty length is useful, but it should not be the only decision factor. Buyers should also review spare-parts availability, technical response time, operator retraining support, abrasive resupply, and the supplier’s ability to adjust process parameters after commissioning. For a batch wet blasting machine, stable after-sales support is closely tied to long-term consistency, not just to repair coverage.