Quick Answer
Automated deburring is the use of controlled machine-based finishing to remove burrs, feather edges, recast layers, and micro-protrusions from metal parts with far better consistency than manual methods. In wet blasting systems, abrasive media is suspended in water, accelerated by compressed air, and applied under repeatable pressure and motion control. That makes the process especially suitable for precision parts, finish-sensitive surfaces, and production lines that need stable edge quality, lower dust, and predictable cycle times.
| Core Factor | Typical Conclusion |
|---|---|
| Process type | Wet blasting / slurry blasting with automated nozzle or part motion |
| Pressure control | Typically low-to-medium blasting pressure with closed-loop regulation |
| Accuracy potential | High repeatability when servo motion and recipe control are used |
| Dust behavior | Low airborne dust because the abrasive is carried in water |
| Primary applications | Burr removal, edge blending, coating pretreatment, tool edge preparation |
| Lead-time band | Typical lead time depends on cabinet size, automation scope, and fixturing |
What Is Automated Deburring
Automated deburring is the machine-controlled removal of unwanted material left on a part edge after machining, stamping, punching, laser cutting, broaching, grinding, forging, or additive manufacturing. The objective is not simply to make a part feel less sharp. In modern production, deburring also protects dimensional fit, coating adhesion, assembly quality, handling safety, and final inspection accuracy.
Within the broader surface-treatment field, automated deburring can include brushing, belt finishing, thermal deburring, vibratory finishing, electrochemical processes, and abrasive blasting. Wet blasting belongs to the abrasive-blasting family, but it differs from dry blasting because the abrasive is suspended in water rather than propelled as a fully dry stream. That water phase changes impact behavior, dust generation, media recovery, and finish quality.
Where Automated Deburring Fits in Wet Blasting
In slurry blasting, burr removal is often combined with edge softening and cosmetic surface equalization. Instead of attacking the workpiece with a dry, highly aggressive stream, the process uses a cushioned abrasive impact that can trim thin burrs while preserving nearby geometry. For many parts, that makes automated deburring a finishing step rather than a stock-removal step.
This matters because most production burrs are small but consequential. A minor lip on a valve bore, a feather burr on a stamped bracket, or a rough support-contact zone on an additively manufactured part may not require heavy grinding, but it can still cause sealing issues, coating defects, or assembly interference. Automated wet blasting is often selected for exactly this middle ground.
Core Benefits of Automated Deburring by Slurry Blasting
One important benefit is dust-free operation relative to dry abrasive processes. Water suppresses airborne fines and reduces the housekeeping burden around the machine, which is valuable in plants where cleanliness and operator visibility matter.
Another is no media embedding in many finish-sensitive applications. Because the water film cushions impact, the risk of forcing abrasive particles into softer or more ductile surfaces is often lower than with dry blasting. That can be relevant before coating, brazing, optical inspection, or cosmetic finishing.
A third benefit is finish quality. Wet blasting tends to produce a finer and more uniform surface because the abrasive action is moderated by the slurry phase. On precision parts, that can help deburr edges without leaving the harsh texture sometimes associated with more aggressive dry processes. General process terminology for this family is consistent with abrasive blasting terminology.
Why Manufacturers Automate Deburring Instead of Relying on Hand Work
Manual deburring still has a place, especially for prototypes or oversized burrs. But it is difficult to control across operators, shifts, and production lots. Two technicians can produce visibly different edge conditions on the same part, and fatigue tends to increase variation over time.
Automation addresses that problem by defining pressure, nozzle angle, stand-off distance, traverse speed, and cycle time as controlled variables. Once the recipe is validated, the machine repeats the same logic across every batch. The result is process repeatability, which is often more valuable than raw removal speed.
The most effective deburring line removes the burr without creating a new geometry or surface defect.
How Does Automated Deburring Work
Automated deburring by wet blasting works through a coordinated sequence of slurry preparation, compressed-air acceleration, controlled nozzle or part motion, and closed-loop recovery. Each subsystem affects the final edge condition. If any one variable drifts, burr-removal performance becomes less stable.
Slurry System: Water Plus Abrasive in Suspension
The process begins with a slurry tank where water and abrasive media are mixed to a controlled concentration. Agitation and circulation keep the particles suspended so that the abrasive content reaching the gun remains consistent over time. If the slurry becomes too dilute, burr-removal efficiency drops; if it becomes too concentrated, finish roughness, pump load, and media consumption can increase.
Media selection depends on burr thickness, substrate hardness, allowable edge break, and target appearance. Finer media is generally used for precision deburring and surface refinement, while coarser media increases cutting action but can over-round delicate edges if not controlled carefully.
Compressed-Air Acceleration Path
At the blasting gun, compressed air accelerates the slurry through a nozzle and directs it toward the workpiece. The water phase helps distribute the abrasive stream more evenly and cushions the particle impact. This changes the mechanism from aggressive dry cutting to a more moderated micro-erosion process.
Stand-off distance and nozzle angle matter as much as pressure. A near-normal impact angle tends to increase local removal intensity, while an oblique angle can be better for feather burr trimming and edge blending. Automated systems hold these variables far more consistently than manual hand guns.
Motion Control in Automated Deburring
In an automated cell, the machine can move the nozzle, the workpiece, or both. This is typically done through servo-driven linear axes, rotary tables, robots, or dedicated fixtures. The right motion architecture depends on part geometry: flat plate-shaped parts may need scanning passes, cylindrical parts may need rotational exposure, and complex parts may need multi-axis toolpaths.
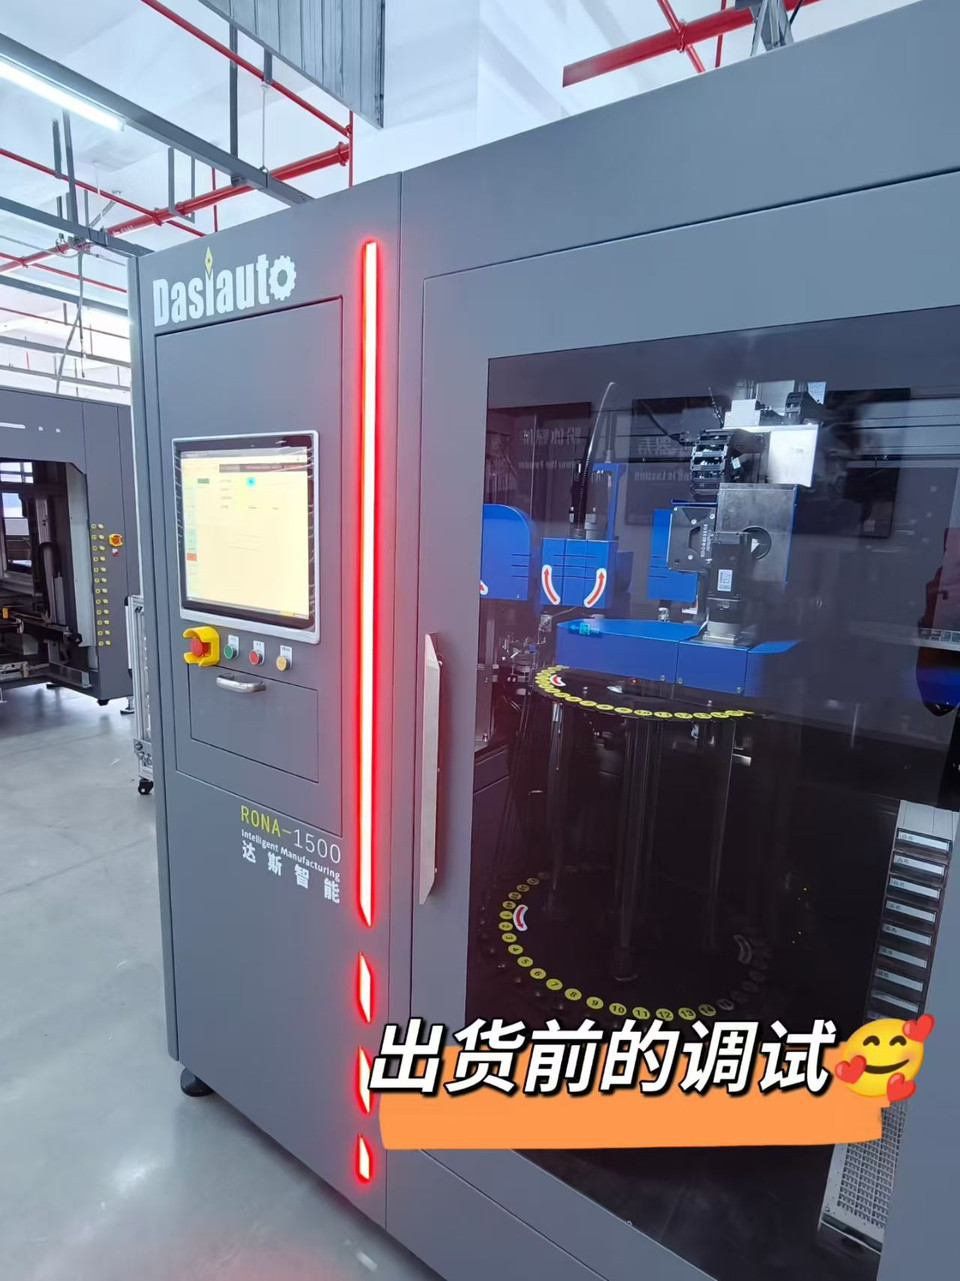
For finish-critical work, programmed motion is essential. It lets the process apply equal exposure to every edge instead of relying on operator judgment. DasiAuto’s application-specific work in burr removing of metal parts reflects this selective, path-controlled approach rather than a one-size-fits-all blasting routine.
Closed-Loop Recovery and Sedimentation
After impact, the slurry falls into the recovery section of the machine and is routed back into the circulation loop. Removed burr fragments, fines, and worn abrasive must be separated so they do not destabilize the process. In more advanced systems, waste sand settles through a sedimentation stage and is discharged automatically, reducing manual cleanup and helping preserve usable media.
This recovery loop is one of the main engineering distinctions between a simple blast cabinet and a production-grade wet blasting system. Efficient circulation supports stable concentration, lower media waste, and shorter cleaning downtime. It also reduces the chance that broken media or metallic debris will alter finish quality from batch to batch.
Mist Control and Chamber Management
Although wet blasting minimizes dry dust, it still requires mist management. Water droplets and fine slurry aerosol can accumulate inside the chamber if extraction, drainage, and cabinet sealing are poor. Production equipment therefore combines mist reduction, splash management, visibility control, and enclosed material handling.
That combination matters in automated deburring because cycle times are only meaningful if the chamber remains clean and viewable enough to sustain production. Low-maintenance mist control also reduces interruptions related to window cleaning, sludge buildup, and floor contamination around the machine.
Pressure Stability and Recipe Control
The blasting effect depends on consistent energy delivery. If pressure drifts, the same nozzle path can produce different edge conditions from the beginning to the end of a production run. That is why PID closed-loop pressure control is so important in industrial wet blasting.
With PID control, the machine continually adjusts output to stay near the target setpoint. That improves consistency during long runs and helps compensate for normal process disturbances such as nozzle wear or slurry-state variation. HMI recipe management then stores the validated settings by part family, reducing setup variability and supporting operator permissions and traceability under systems aligned with the ISO 9001 quality management standard.
| Process Parameter | Typical Range or Practice | Why It Matters |
|---|---|---|
| Working pressure | Typically low to medium, adjusted to burr size and substrate hardness | Controls removal intensity and edge-break behavior |
| Slurry concentration | Usually maintained as a stable water-to-abrasive ratio by weight or volume | Affects finish consistency, media usage, and deburring rate |
| Abrasive particle size | Fine to medium PSD, chosen for precision vs. cutting balance | Determines how aggressively the burr root is attacked |
| Air flow and nozzle size | Matched to gun design, cabinet size, and coverage width | Influences stream energy and pattern stability |
| Stand-off distance | Fixed as a recipe variable for each part family | Changes impact density and local removal effect |
| Nozzle angle | Normal or oblique depending on burr orientation | Determines whether the process cuts, blends, or lightly peens |
| Media consumption | Varies with fracture rate, contamination, and recovery efficiency | Drives operating cost and maintenance intervals |
| Control system | Closed-loop pressure, HMI recipes, alarms, recovery monitoring | Supports stable automated deburring across batches |
Automated Deburring vs Dry Blasting vs Other Methods
Automated deburring is not a single technology category. Buyers often compare wet blasting against dry blasting, shot peening, and vibratory finishing because all four can change an edge or surface. The real question is not which one is universally best, but which one fits the burr type, finish requirement, and production model.
| Evaluation Factor | Wet Blasting | Dry Blasting | Shot Peening | Vibratory Finishing |
|---|---|---|---|---|
| Dust generation | Low airborne dust due to water-carried media | High unless dust extraction is robust | Moderate; depends on enclosure and media | Low airborne dust but often involves wet compounds and sludge |
| Finish uniformity | Generally fine and even on visible surfaces | More aggressive texture, can be less forgiving | Surface change is secondary to residual stress intent | Good on bulk loads, but less selective |
| Media embedding risk | Lower in many finish-sensitive applications | Higher risk on some soft or ductile materials | Depends on media and substrate | Usually low, but part-to-part contact can mark surfaces |
| Deburring selectivity | Good with controlled nozzle path and fixtures | Good targeting, but easier to over-process | Not primarily intended for burr removal | Low selectivity because all exposed surfaces are processed together |
| Repeatability | High with closed-loop pressure and recipe control | Good, but dust and nozzle wear can shift conditions | High when peening specs are tightly controlled | Good for bulk parts, weaker for critical localized edges |
| Environmental handling | Requires slurry management and sediment removal | Requires dust collection and dry media containment | Requires media handling and enclosure controls | Requires water, compounds, and waste-slurry handling |
| Best-fit role | Precision deburring, edge blending, coating prep | Aggressive cleaning, roughening, or heavy surface attack | Fatigue-oriented treatment; see shot peening reference | Batch smoothing of small non-critical parts |
| Cost structure | Equipment and controls matter; operating cost tied to media loop | Simpler blasting hardware, but more dust burden | Specialized when performance specs are strict | Efficient for high-volume small parts with simple geometry |
Dry blasting still has a role where aggressive cleaning, coating removal, or heavy surface roughening is the main objective. For delicate edges, however, it can be easier to over-process the part or leave a rougher cosmetic outcome than intended. Wet blasting is usually preferred when the finishing objective includes both burr removal and appearance control.
Shot peening is sometimes mentioned in the same conversation, but its primary purpose is surface stress conditioning rather than burr removal. Industry specifications and terminology for peening are addressed in technical documents such as ASTM standards resources, and those requirements are usually different from deburring objectives.
Vibratory finishing is efficient for high-volume small parts, especially when all surfaces can tolerate similar exposure. Its limitation is that it is a mass-finishing process rather than a selective one. For critical edges, sealing lands, or parts that cannot contact each other freely, automated wet blasting is often easier to control.
Key Specifications to Evaluate Before Buying
The most common procurement mistake in automated deburring is buying on machine size before defining the burr condition. A line designed for heavy oxide removal is not necessarily right for feather-burr trimming on precision machined parts. Buyers should begin by documenting burr type, burr location, allowable edge break, target surface finish, and downstream process sensitivity.
Blasting Pressure Window
A useful machine must hold the pressure range the part actually needs, not just advertise a high maximum. Precision wet blasting usually depends on a stable low-to-medium pressure band where removal remains controllable. Ask how the system compensates for pressure drift, nozzle wear, and slurry-state changes during extended operation.
Motion-Axis Accuracy and Part Handling
Motion accuracy is critical when the burr is local, the part is small, or the geometry is complex. Evaluate whether the machine uses manual manipulation, indexed fixtures, servo X/Y/Z motion, or robot-assisted loading. If path precision affects the result, the control architecture should be reviewed as carefully as the pump or nozzle.
Throughput and Cycle Discipline
Throughput is more than blast time. Loading, unloading, fixturing, drainage, cleaning, recipe calling, and chamber recovery can consume as much time as the abrasive step itself. Procurement teams should compare true cycle time per good part, not just nozzle exposure seconds.
Workspace Footprint and Utilities
Wet blasting equipment requires floor space, compressed air, electrical supply, water management, drainage, and maintenance access. A cabinet that technically fits in the room may still be a poor installation choice if sludge discharge, nozzle replacement, or pump servicing is difficult.
HMI, Recipe Control, and Traceability
Recipe storage is essential when multiple part families share a line. The best systems let users lock key variables, assign permissions, and recall validated settings without manual re-entry. That reduces startup variation and supports process discipline when operators change by shift.
Mist Control, Waste-Sand Handling, and Housekeeping
Because automated deburring is a continuous process, maintenance design matters. Buyers should assess sedimentation logic, sludge discharge, viewing-window cleanliness, mist extraction, and the time needed to recover from media contamination. A technically capable blast path can still become inefficient if the recovery system is weak.
Safety and Compliance
Door interlocks, emergency stops, chamber sealing, exposure control, ergonomic loading height, and utility isolation should be reviewed early. Where deburring is part of pretreatment before painting or corrosion protection, some plants also benchmark against broader surface-preparation guidance from AMPP surface preparation practices.
Applications Across Industries
Automated deburring is valuable because burrs are not industry-specific; they are a byproduct of almost every metal-cutting and forming process. What changes from sector to sector is the tolerance for edge damage, contamination, cosmetic inconsistency, and variable manual labor.
| Application Type | Target Industry | Workpiece Example | Process Benefit |
|---|---|---|---|
| Edge honing of cutting tools | Carbide tool manufacturing | Inserts, drills, end mills | Stabilizes cutting edge condition and reduces micro-chipping risk |
| Burr removing of metal parts | Precision machining, stamping, and fabrication | Housings, clips, brackets, valve bodies | Removes sharp burrs without heavy stock loss |
| Scale removal from forgings or bars | Forging and primary metal processing | Forged fittings, steel bars, heat-treated parts | Cleans oxide and supports downstream machining or coating |
| Pretreatment before coating | Automotive, hardware, and general fabrication | Sheet-metal parts, enclosures, welded assemblies | Improves cleanliness and surface consistency before paint or phosphating |
| Post-processing of AM parts | Additive manufacturing | Printed brackets, manifolds, support-contact zones | Reduces roughness and removes loose residues on complex geometries |
| Peening of metal parts | Mechanical component production | Springs, gears, selected fatigue-sensitive parts | Adds controlled surface impact when peening is also required |
| Glass frosting | Architectural and consumer products | Glass covers, decorative panels | Produces even matte texture with controlled visual finish |
| 3C device finishing | Consumer electronics supply chain | Frames, shells, cosmetic metal components | Delivers uniform smoothness on visible surfaces |
In cutting-tool production, deburring often overlaps with controlled edge preparation. A process that merely removes burrs may still fail if it leaves an unstable cutting edge. That is why many toolmakers assess automated deburring alongside edge honing of cutting tools when defining the final surface-treatment route.
Coating lines are another strong fit because uncontrolled burrs can create thin-film breaks, local corrosion points, and handling hazards. For parts moving directly into paint or conversion treatment, coating pretreatment wet blasting can align burr control with surface cleanliness in a single upstream step.
Additive manufacturing adds a different challenge: irregular surfaces, trapped residues, and complex internal-adjacent features. Wet blasting is useful here because it combines cleaning and surface moderation without the dry-dust burden of conventional blasting. The process still requires careful validation, especially for thin walls, lattice edges, and unsupported projections.
Equipment Selection Guide
Selecting the correct equipment configuration begins with three questions: How many parts per shift must be processed, how consistent must the edge condition be, and how complicated is the part geometry? Those answers usually determine whether a simple cabinet is enough or whether the plant needs multi-axis automated deburring with dedicated fixtures and higher-level controls.
| Configuration / Model Tier | Target Production Scale | Workpiece Size Range | Precision Level | Recommended Applications |
|---|---|---|---|---|
| R&D lab-scale robot cell | Trials, validation, small batches | Small to medium complex parts | High | Process development, sample testing, flexible part programs |
| Manual single-piece wet blasting unit | Low-volume production | Small to medium single parts | Medium to high | Individual parts, mixed production, finish-sensitive components |
| Standard single-chamber batch cabinet | Routine batch production | Small to medium repeat parts | Medium | Daily deburring, edge softening, general finish equalization |
| Double-chamber production system | Higher-output batch production | Small to medium repeat parts | Medium | Overlapped loading and blasting for better utilization |
| Servo multi-axis precision system | Critical edge control | Small complex geometries | Very high | Tool edge prep, local deburring, repeatable precision finishing |
| Complex-shape dedicated system | Engineered production cells | Medium complex parts | High | Recessed surfaces, contoured parts, multi-angle exposure |
| Plate-shaped parts machine | Flat and panel-like work | Medium to large flat parts | Medium to high | Sheet parts, covers, decorative faces, uniform surface scanning |
| Round-rod or bar-stock line | Continuous or semi-continuous work | Long cylindrical parts | Medium | Bar descaling, circumferential cleanup, rod surface conditioning |
For pilot projects and new product introduction, a flexible R&D platform is often the best starting point because abrasive type, nozzle path, and fixturing can be adjusted quickly. In that context, the RB-6 robot-type wet blasting equipment fits process development and sample validation better than a fixed high-throughput line.
For mainstream batch production, a standard cabinet is usually more economical and easier to integrate. A plant that needs balanced output without complex part motion may evaluate an SC-40 single-chamber wet blasting cabinet, while higher-loading rhythms may warrant evaluation of a DC-40 double-chamber blasting system. Confirm model suitability on representative parts and verify any reduction in idle time through a cycle study.
Configuration should also reflect part presentation. Single-piece handling is useful for cosmetic or fragile components; plate-shaped parts benefit from wide scanning coverage; complex shapes often require multi-angle access; and round stock needs rotational exposure. In other words, automated deburring is as much about motion and fixturing as it is about abrasive energy.
Cost, Lead Time and ROI Considerations
The cost of automated deburring equipment is driven primarily by control complexity, not only by cabinet size. Automation level, number of motion axes, slurry-circulation design, recovery system, HMI capability, fixturing, and mist control all shape capital cost. Two machines can look similar externally while having very different long-term performance and maintenance burdens.
Abrasive strategy also affects total cost of ownership. Media type, particle-size stability, fracture rate, contamination sensitivity, and recyclability all influence operating cost. Cheaper media may raise the real process cost if it breaks down quickly, shortens nozzle life, or makes finish results less predictable.
Lead time is usually shortest for standard machines and longest for application-specific automated cells. Once sample testing, fixture design, custom guarding, motion programming, and factory acceptance criteria are added, project schedules become more dependent on engineering scope than on metal fabrication alone. Buyers should therefore distinguish between typical standard-platform lead times and fully customized system lead times.
Typical Price Drivers in Automated Deburring
The first cost driver is machine architecture. A manually loaded cabinet with simple indexing is inherently different from a servo multi-axis precision cell with recipe traceability and integrated sludge handling. The second is process validation, because high-value parts often require extensive testing before equipment configuration is frozen.
Third, auxiliary systems matter. Mist extraction, automatic waste-sand sedimentation, recipe-capable HMI, inspection fixtures, and part-specific holders all influence both cost and uptime. Plants should avoid comparing quotations unless the same accessories and acceptance scope are included.
How to Frame ROI Correctly
ROI is strongest when automated deburring replaces labor-intensive hand finishing with inconsistent results. But the savings do not come only from labor. Stable edge condition can reduce rework, lower scrap, improve assembly fit, improve coating performance, and reduce inspection disputes between departments.
In cutting-tool applications, a controlled edge can also improve tool-life consistency rather than only removing residual burrs. In coating applications, the benefit may appear as better adhesion and fewer local failures. In precision machining, the biggest gain may simply be fewer downstream issues caused by one missed burr on a high-value part.
Why Manual-Cost Comparisons Are Often Misleading
Manual deburring is frequently underestimated because hidden losses are distributed across labor, quality, and maintenance budgets. When a plant tracks only direct operator time, it misses the cost of inconsistent edge quality, ergonomic strain, training variance, missed burrs, part damage, and inspection delays. Automated deburring often becomes economically justified once those secondary costs are measured.
A disciplined ROI review should therefore compare total process performance: good parts per hour, rework rate, operator dependency, consumables, maintenance intervals, and downstream quality effects. That is a more realistic basis for investment than quoting a machine against a single hourly wage figure.
Why Choose DasiAuto?
Established in 2012, DasiAuto develops and manufactures wet blasting equipment for industrial surface treatment. The company brings together equipment engineering, abrasive media, and application development, as described in About DasiAuto.
Application testing and process development help evaluate abrasive media and treatment settings before the equipment configuration is defined. Equipment engineering can bring together the blasting system, fixtures, automation, and part handling around the application.
Suitability for a particular material, geometry, finish, or dimensional requirement needs to be established through representative sample testing. DasiAuto supports installation, operator training, and ongoing technical support through the production workflow.
FAQ
Can Automated Deburring Be Validated With Sample Parts Before Ordering Equipment?
Yes. Sample testing is usually the most reliable way to confirm burr-removal capability, surface finish, cycle time, and fixture suitability before finalizing the machine scope. It also helps determine whether the part needs simple batch exposure or more precise nozzle-path programming.
Is Automated Deburring Suitable for High-Mix, Low-Volume Production?
It can be, provided the machine supports fast recipe changeover and practical fixturing. High-mix production benefits most when part programs, pressure settings, and motion paths can be stored and recalled without lengthy manual setup.
What Utilities and Installation Conditions Should Buyers Review in Advance?
Compressed air, electrical supply, water management, drainage, maintenance access, and floor space should all be checked before purchase. Wet blasting systems also need practical plans for mist control, sediment removal, and safe loading ergonomics.
How Much Operator Training Does an Automated Deburring System Typically Require?
Training usually focuses on recipe selection, fixture loading, slurry maintenance, nozzle inspection, chamber cleaning, and process troubleshooting. Even with automation, operators still need to recognize the difference between acceptable edge blending, under-processing, and over-rounding.
What Spare Parts and Consumables Matter Most in Long-Term Operation?
Nozzles, pumps, seals, filters, wear liners, and abrasive media are the most common planning items. Buyers should also ask how slurry condition is monitored and how often recovery-system cleaning is required to keep automated deburring stable over time.
When Does Automated Deburring Usually Pay Back Faster Than Manual Deburring?
It usually pays back faster when parts are repetitive, quality-sensitive, labor-intensive, or difficult to deburr consistently by hand. The strongest business case appears when missed burrs, finish variation, rework, or downstream coating and assembly issues are already creating measurable production losses.